How to Choose the Best Tin Bar Casting Machine?
Choosing the right Tin Bar Casting Machine requires more than comparing prices, power ratings, or production claims. The machine must match your alloy, bar dimensions, output target, and working environment. A small workshop may need a compact unit with simple controls. A high-volume facility may require automated feeding, stable temperature regulation, and continuous cooling. These differences affect product quality every day.
Look closely at the melting system, mold design, casting speed, and temperature accuracy. A variation of only a few degrees can influence surface finish, shrinkage, and bar consistency. Inspect the control panel, cooling channels, extraction system, and emergency shutdown features. Ask suppliers for verified data, maintenance schedules, and references from comparable operations. Practical testing is valuable. Request sample bars, if possible, and examine their edges, weight, and surface texture.
No machine is perfect.
A lower-cost model may seem attractive, yet frequent cleaning or manual adjustment can reduce real productivity. An advanced machine may improve consistency, but its software and spare parts could require specialized support. I have seen buyers focus on maximum capacity while overlooking installation space and operator training. That mistake can become expensive. Consider energy consumption, replacement components, technical service, and long-term reliability before deciding. This guide explains how to compare each factor with a professional, evidence-based approach. It also recognizes an uncomfortable truth: supplier brochures rarely show every limitation. Careful questions, factory inspection, and realistic production trials often reveal more than impressive specifications.
Define Your Tin Bar Production Requirements
How to Choose the Best Tin Bar Casting Machine?
Define Your Tin Bar Production Requirements
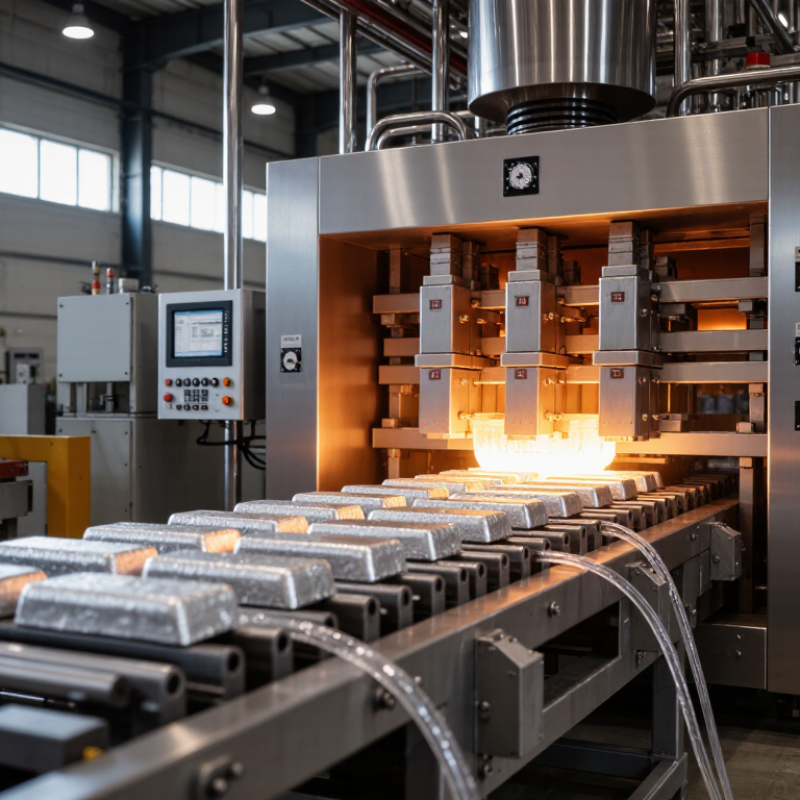
Choosing a tin bar casting machine starts with your actual production plan, not its advertised capacity. Record your target output per hour, bar weight, length, width, and acceptable dimensional tolerance. A small workshop may need 100 kilograms daily, while a continuous line may require several tonnes. These are completely different purchasing decisions.
Measure the melting temperature range and confirm the material composition you will process. Tin alloys can respond differently to heat, cooling speed, and mold design. The machine should provide stable temperature control, even metal flow, and sufficient cooling time. Ask for heating accuracy, mold replacement time, and energy consumption data. In practice, these details affect production more than appearance.
Consider your operators and factory layout. Check the machine footprint, loading method, ventilation needs, and access for maintenance. Automatic bar cutting can improve consistency, but it may increase setup complexity. A larger machine is not always better. That assumption can fail. Choose controls that workers can understand quickly, with clear alarms and accessible emergency stops. Confirm inspection records, electrical protection, and compliance with applicable industrial standards. Request sample casting results using your intended alloy and bar dimensions. One trial may reveal shrinkage, surface marks, or uneven edges that brochures cannot show. Leave room for future demand, but avoid paying for capacity you cannot use.
How to Choose the Best Tin Bar Casting Machine?
Define your tin bar production requirements before comparing machine capacity, mold configuration, and automation level.
This planning example assumes a target output of 1,200 kg per day and 8 productive operating hours per shift, equal to an average requirement of 150 kg per hour. A machine should provide additional capacity above this average to accommodate melting, pouring, mold changes, cooling, and maintenance downtime. For example, producing 5 kg bars requires approximately 30 bars per hour, while producing 20 kg bars requires approximately 7.5 bars per hour.
Evaluate Capacity, Precision, Energy Use, and Material Compatibility
How to Choose the Best Tin Bar Casting Machine?
Capacity should match your actual production rhythm, not an optimistic sales forecast. A machine producing 500 kilograms daily may struggle with your alloy, mold size, or cooling schedule. Check hourly output under similar conditions. Ask for test data, not only maximum ratings. Precision matters when bars must meet tight weight and dimensional limits. Review temperature control, mold alignment, automatic pouring accuracy, and calibration records. Even a small temperature fluctuation can create surface cracks or uneven grain structures.
Tips: Test a sample batch before purchasing. Measure bar weight, length, surface finish, and rejection rates. Record energy use during heating, holding, casting, and cooling. This reveals the real operating cost. Insulation quality, heating control, and standby consumption deserve attention. Lower energy use is helpful, but poor thermal stability can increase waste. I once underestimated cooling demand during a production trial. The machine performed well initially, then lost consistency after several hours.
Material compatibility should be confirmed with your tin grades, additives, and recycled content. Ask about crucible materials, pump design, mold coatings, and cleaning requirements. Some components tolerate pure tin but wear faster with certain mixtures. Request maintenance intervals and replacement-part specifications. A practical supplier should explain limitations clearly and support process verification. Do not choose by capacity alone. The best machine fits your material, floor space, operators, and quality controls. There is always a compromise. Make it visible before signing.
How to Choose the Best Tin Bar Casting Machine? — Evaluate Capacity, Precision, Energy Use, and Material Compatibility
Comparison of typical machine configurations for tin and tin-alloy bar production
| Machine Configuration | Typical Output
(kg/h) | Melt Capacity
(kg) | Temperature Range
(°C) | Bar Weight
Tolerance | Specific Energy Use
(kWh/t) | Recommended Bar
Dimensions | Compatible Materials | Best Use Case |
| Compact batch caster | 15–40 | 30–80 | 250–450 | ±1.0–2.0% | 140–220 | 10–40 mm wide
10–30 mm thick | Pure tin, low-antimony tin, selected lead-free alloys | Laboratories, pilot production, frequent alloy changeovers |
| Standard continuous caster | 50–120 | 100–250 | 250–500 | ±0.5–1.0% | 110–180 | 15–60 mm wide
10–40 mm thick | Pure tin, tin-copper, tin-antimony, common lead-free solder alloys | General-purpose industrial bar production |
| High-throughput continuous line | 150–400 | 300–800 | 250–550 | ±0.3–0.7% | 90–160 | 25–100 mm wide
15–60 mm thick | Pure tin and stable-composition tin alloys with controlled feeding | High-volume production with long operating cycles |
| Precision servo-controlled caster | 30–150 | 80–350 | 250–450 | ±0.2–0.5% | 120–200 | 10–80 mm wide
8–50 mm thick | Pure tin, solder alloys, tin-copper, tin-silver and tin-antimony alloys | Tight dimensional control and reduced downstream machining |
| Induction-heated caster | 60–250 | 120–500 | 250–600 | ±0.4–0.8% | 80–150 | 20–90 mm wide
15–55 mm thick | Pure tin and conductive tin alloys; crucible and coil must suit alloy chemistry | Fast heat-up, responsive temperature control and lower standby losses |
| Heavy-duty alloy caster | 100–300 | 250–700 | 300–650 | ±0.5–1.0% | 130–230 | 30–120 mm wide
20–70 mm thick | Tin-lead, tin-antimony and other alloys requiring robust refractory contact surfaces | Long campaigns, larger bars and demanding thermal duty |
Capacity check
Select a rated output at least 15–25% above the required average production rate to accommodate start-up, cleaning, temperature recovery and material changes.
Precision check
Confirm whether the stated tolerance applies to individual bar weight, cross-section, length or the complete batch. Ask for acceptance samples using the intended alloy.
Energy check
Compare specific energy consumption in kWh per tonne under the same alloy, output rate, holding temperature and operating schedule.
Material compatibility
Verify crucible, pump, mold, coating and wetted-metal materials. Lead-containing alloys also require suitable ventilation, handling procedures and regulatory controls.
Note: Values are representative engineering ranges for properly maintained equipment and may vary with bar geometry, alloy composition, cooling method, casting speed, furnace insulation and factory utilities. Tin melts at approximately 232°C; operating temperatures are normally set above the liquidus temperature to maintain stable flow without excessive oxidation.
Assess Supplier Support, Total Cost, and Long-Term Value
When choosing the best tin bar casting machine, supplier support deserves more attention than glossy specifications. During plant evaluations, I check how quickly the supplier answers technical questions. A fast reply matters. Ask about installation, operator training, troubleshooting, and spare-part availability. Request clear manuals and a realistic commissioning schedule. If a supplier cannot explain maintenance intervals, support may become difficult after delivery.
Total cost extends far beyond the purchase price. Include electricity use, cooling requirements, mold changes, labor, maintenance, and rejected bars. Ask for hourly energy data under similar production conditions. Calculate costs over five years, not five weeks. My first cost model once underestimated technician travel and replacement sensors. Estimates are never perfect. Leave room for price changes, downtime, and production growth. A longer warranty can help, but only when its response terms are written clearly.
Long-term value depends on stable performance and practical upgrade options. Review service records from comparable installations, not only customer testimonials. Ask whether the control system can receive future improvements without replacing the entire machine. Check casting consistency by examining sample bars, surface finish, dimensions, and defect rates. Do not trust polished brochures alone. A machine with a low price may become expensive if support is slow or parts are unavailable. Supplier financial stability also matters. Good equipment should support safe, repeatable production for many years.